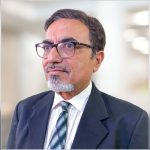
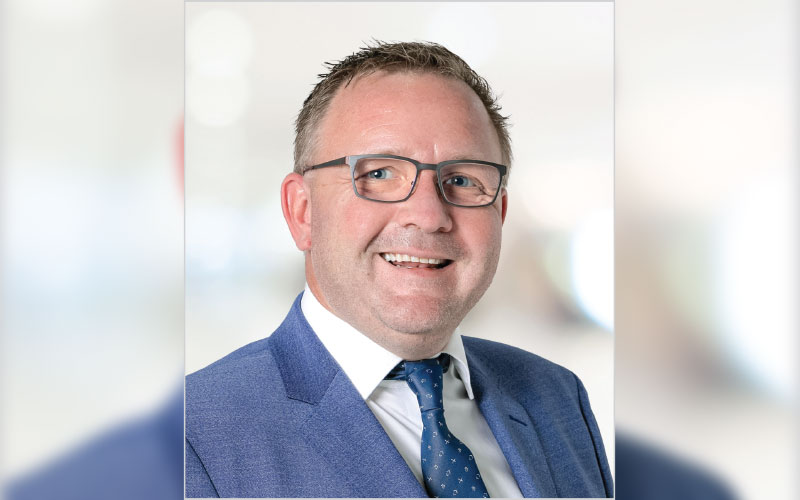
Rosendahl Nextrom is advancing cable extrusion technology by combining process engineering, automation, digital monitoring and material expertise. As cable manufacturers demand higher speeds, tighter tolerances and greater product flexibility, the company focuses on stable processing, faster changeovers and reduced scrap. In an exclusive interaction with Wire & Cable India, Mr. Marc Richling, Director – Extrusion Technology, Rosendahl Nextrom, talks about how they integrate machine design, controls and data architecture while addressing the specific processing requirements of HFFR, LSZH, XLPE, elastomers and high-performance polymers. Laboratory testing, material collaboration and application-specific engineering further support reliable production and shorter development cycles. Looking ahead, Rosendahl Nextrom sees AI-assisted control, simulation and connected process data shaping the next generation of extrusion machinery.
Wire & Cable India: Cable manufacturers today produce an increasingly diverse range of products using different polymers, performance requirements and production speeds. Which developments are placing the greatest demands on modern extrusion systems, and why?
Marc Richling: The greatest demand is no longer maximum output for one product; it is maintaining high output, stable quality and short changeover times across a broad range of polymers and cable designs on the same line. This requires an extrusion system with a wide operating window, simple handling and screw and feeding concepts that remain stable without compromising homogenisation.
Rosendahl Nextrom addresses this through extensive laboratory work and our modular feed concept. Physical foaming raises the bar further: tighter tolerances require highly stable feeding and melt pressure, uniform mixing and precise gas dosing. Low-temperature PP or PE foams are especially challenging because these are often multi-component blends which differ markedly in melting and thermal behaviour. The decisive point is that the complete process must be engineered as one system—the best gas dosing can compensate for neither an unsuitable screw nor an unsuitable polymer, which also underlines the importance of polymer selection. This holistic approach gives customers the flexibility to run more products, change over faster and still achieve consistently high quality.
Watch: Top Cable Companies in India
WCI: Compared with five years ago, which aspects of the extrusion process have become technically more difficult to control consistently? How have machinery design and process engineering evolved to address these challenges?
MR: Compared with five years ago, the increasing number of shaped, non-round and special products has made material flow through the tooling much more difficult to control. Small flow imbalances can quickly affect geometry, wall-thickness distribution and surface quality. The answer is a stronger combination of flow simulation, accurate material characterisation and practical validation. We work closely with material manufacturers and often evaluate new compounds at a very early stage, which gives us better data for designing screws, crossheads and tooling. By combining simulation with trials on our laboratory lines, we reduce development loops, shorten time to market and give customers more predictable results. Software is becoming increasingly important, but it creates real value only when it is backed by deep process know-how.
WCI: Modern cable compounds such as HFFR, LSZH, XLPE, specialised elastomers and engineering polymers each present unique processing characteristics. Which material-related challenges are driving the most significant innovations in extrusion equipment today?
MR: The guiding principle is simple: every polymer must be treated according to its specific behaviour. With HFFR and other highly filled compounds, the challenge is to combine high output with sufficient plasticisation, low melt temperature and good homogeneity while minimising plate-out. Thermoplastic elastomers such as TPE-U and TPE-C require gentle processing because excessive shear can damage their morphology. XLPE demands a self-cleaning, carefully designed flow path to prevent pre-crosslinking and surface defects. High-performance polymers such as PPSU, PEEK and TPI also require disciplined material handling, including thorough drying and, in some cases, inert-gas conditions. Through early cooperation with material manufacturers and application testing in our laboratories, Rosendahl Nextrom develops the correct processing window before a material reaches broad production. This material know-how is essential for quality, uptime and long cleaning intervals.
Compared with five years ago, the increasing number of shaped, non-round and special products has made material flow through the tooling much more difficult to control. Small flow imbalances can quickly affect geometry, wall-thickness distribution and surface quality. The answer is a stronger combination of flow simulation, accurate material characterisation and practical validation.
WCI: Customers increasingly expect higher line speeds together with tighter quality tolerances. In practice, where do machinery builders encounter the greatest trade-offs between productivity, process stability and product quality, and how are these being addressed?
MR: The main trade-off appears when higher speed amplifies even small fluctuations in material properties or production conditions. Mechanical precision alone is therefore not enough. Stable extrusion must be combined with automated, closed-loop process control that continuously uses product measurements to keep dimensions within tolerance. At Rosendahl Nextrom, we design the machine, controls and data architecture as one system, allowing customers to increase output without losing process transparency or quality. Digital monitoring also provides full production traceability and can be connected to existing ERP and manufacturing systems. The objective is not simply to run faster, but to produce more saleable cable with less operator intervention, less scrap and consistently high quality.
WCI: Energy efficiency, automation, digital monitoring and process control are widely discussed across the industry. Which of these developments are delivering the greatest measurable operational benefits today, and where do you still see a noticeable gap between industry expectations and practical implementation?
MR: From an operating-cost perspective, process control, digital monitoring and automation currently deliver the greatest measurable benefit because they reduce scrap, raw-material consumption and unplanned downtime—the largest cost factors in many cable plants. Energy efficiency remains important, but its economic impact is often overestimated when viewed in isolation. In many extrusion processes, more than 80% of the energy used to melt the polymer is introduced mechanically through the screw and drive, while the barrel heaters provide the smaller share. A 30% reduction in heater energy would therefore reduce total extrusion energy by only around 6% in this example. The practical gap is that many plants collect data but do not yet convert it into effective automatic control. Our focus is to turn data into stable quality and measurable customer value.
WCI: With cable manufacturers placing increasing emphasis on productivity, quality and operating costs, which factors now have the greatest influence on the investment value of an extrusion line, and how are they shaping machine design and development?
MR: The investment value of an extrusion line is determined far more by total cost of ownership than by purchase price alone. Over the life of the line, raw material, scrap, downtime, changeover time and lost production capacity usually outweigh the initial investment. Machine design must therefore prioritise stable quality, high uptime, flexibility and fast product changes. In one conservative comparison involving a fibre-optic bundling line, the higher initial investment was recovered after approximately 1.5 years through raw-material savings and higher production output. This is the customer-benefit perspective that guides Rosendahl Nextrom: a line should not merely be technically advanced; it should create a measurable economic advantage throughout its operating life.
From an operating-cost perspective, process control, digital monitoring and automation currently deliver the greatest measurable benefit because they reduce scrap, raw-material consumption and unplanned downtime—the largest cost factors in many cable plants.
WCI: As cable manufacturers diversify into sectors such as renewable energy, automotive, EV charging, data communication, railway and specialty cables, how are these applications influencing extrusion line configuration, tooling and overall machine design?
MR: Different applications still require different line configurations, tooling and process conditions. The real engineering challenge is to create customer-specific, multipurpose lines that cover several products without compromising output or quality. That requires more than modular machinery; it requires detailed product, material and process know-how. Rosendahl Nextrom uses application-specific laboratory lines and close cooperation with material manufacturers to test new compounds and cable concepts early. This enables us to react quickly to market developments and configure flexible lines with short changeover times and reliable production windows. We therefore see ourselves not only as a machine supplier, but as a technology and know-how partner that helps customers enter new markets with lower technical risk.
WCI: From your interactions with cable manufacturers, what are the most common misconceptions about extrusion that often lead to avoidable quality issues, inefficiencies or higher production costs? Conversely, what operational practices consistently distinguish high-performing plants?
MR: A common misconception is that extrusion performance can be corrected mainly through machine settings. In reality, the correct choice of extruder concept (such as smooth-bore or grooved-barrel design), screw geometry, material preparation and processing window is decisive. Incorrect selections often result in lower output, unstable quality and higher scrap. High-performing plants treat extrusion as a complete system: they understand their materials, use standardised recipes, plan product sequences intelligently and organise changeovers to minimise cleaning and setup time. They also invest in operator knowledge and use production data to improve the process continuously. For Rosendahl Nextrom, transferring this know-how is part of the solution, because even the best machine delivers its full customer benefit only when technology and operational practice work together.
Also Read: Wire & Cable India Emagazine Sep-Oct Issue 2026
WCI: Looking ahead, which engineering capabilities do you believe will define the next generation of extrusion machinery? Please elaborate from an industry perspective, focusing on the underlying technological and process developments rather than individual product launches.
MR: The next generation of extrusion machinery will connect the entire process digitally—from pellet properties and screw behaviour to melt flow, tooling and final product quality. Greater computing power will enable more holistic simulation, while AI-based assistants and controllers will help operators identify deviations earlier, stabilise production and shorten setup times.
Nevertheless, plastics processing will not become a purely virtual discipline; material data are never perfect, and real compounds must still be validated under production conditions. Technology leadership will therefore depend on combining simulation and automation with laboratory testing, close cooperation with material manufacturers and deep application experience. This is where Rosendahl Nextrom intends to remain ahead: not by developing technology for its own sake, but by translating technical excellence into clear customer value—flexible lines, fast changeovers, low scrap, reliable quality and solutions that are tested early enough to keep customers one step ahead.
The next generation of extrusion machinery will connect the entire process digitally—from pellet properties and screw behaviour to melt flow, tooling and final product quality. Greater computing power will enable more holistic simulation, while AI-based assistants and controllers will help operators identify deviations earlier, stabilise production and shorten setup times.